House Modular Building has rich professional knowledge and experience in the design, engineering, and mass production of premium container houses and prefabricated modular buildings. The company features a highly specialized engineering and design team to provide solution-driven drawings for customized requirements, a dedicated sales and client-success team to manage order logistics, and state-of-the-art factories that guarantee production efficiency, strict structural safety, and timely product delivery.
By blending technological innovation with precision manufacturing, House Modular Building serves as a foundational supplier for construction conglomerates, mining sectors, commercial real estate developers, and international distributors. Our commitment spans from high-grade raw material procurement to modular building block assembly, ensuring that every container unit conforms to strict structural standards and modern architectural designs.
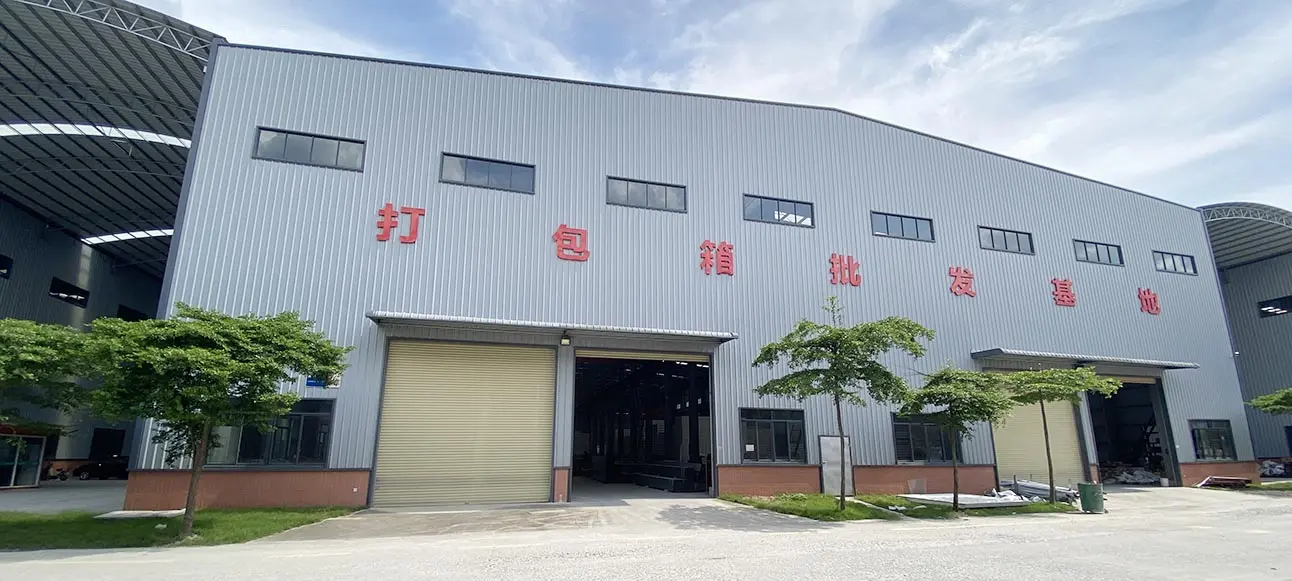
Active Factory Employees
R&D & Engineering Team
Staff with 5+ Years Industry Exp.
Core Leadership Average Tenure
To better serve our global clientele and demonstrate our robust logistics capabilities, we have established production bases in both the North and South of China. This strategic geographic distribution provides efficient and cost-effective delivery routes for customers across various continents, significantly reducing shipping times and ocean freight costs.
Our Northern base optimizes delivery to Northeast Asia, North America, and Europe through northern ports such as Tianjin and Qingdao. Conversely, our Southern base leverages the deep-water ports of Shenzhen and Guangzhou to streamline distribution across Southeast Asia, Oceania, South America, and Africa. We natively support high-capacity OEM and ODM configurations in our factories, allowing international distributors to scale their modular businesses seamlessly via a stable, mutually beneficial partnership.
Direct integration with China’s leading steel mills allows us to source structural Q235 and Q345 hot-dip galvanized steel profiles at lower costs. These savings are directly passed on to our clients, ensuring highly competitive factory-direct pricing without compromising structural integrity.
Our workshops feature automated CNC cutting machines, laser welding units, and electrostatic powder coating lines. This machinery ensures precise tolerances down to the millimeter, accelerating project assembly on-site.
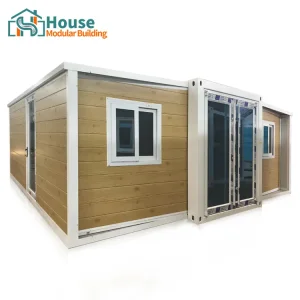
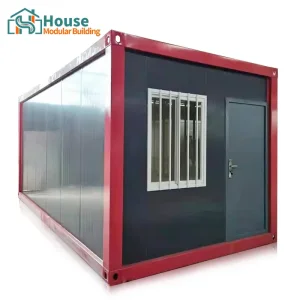
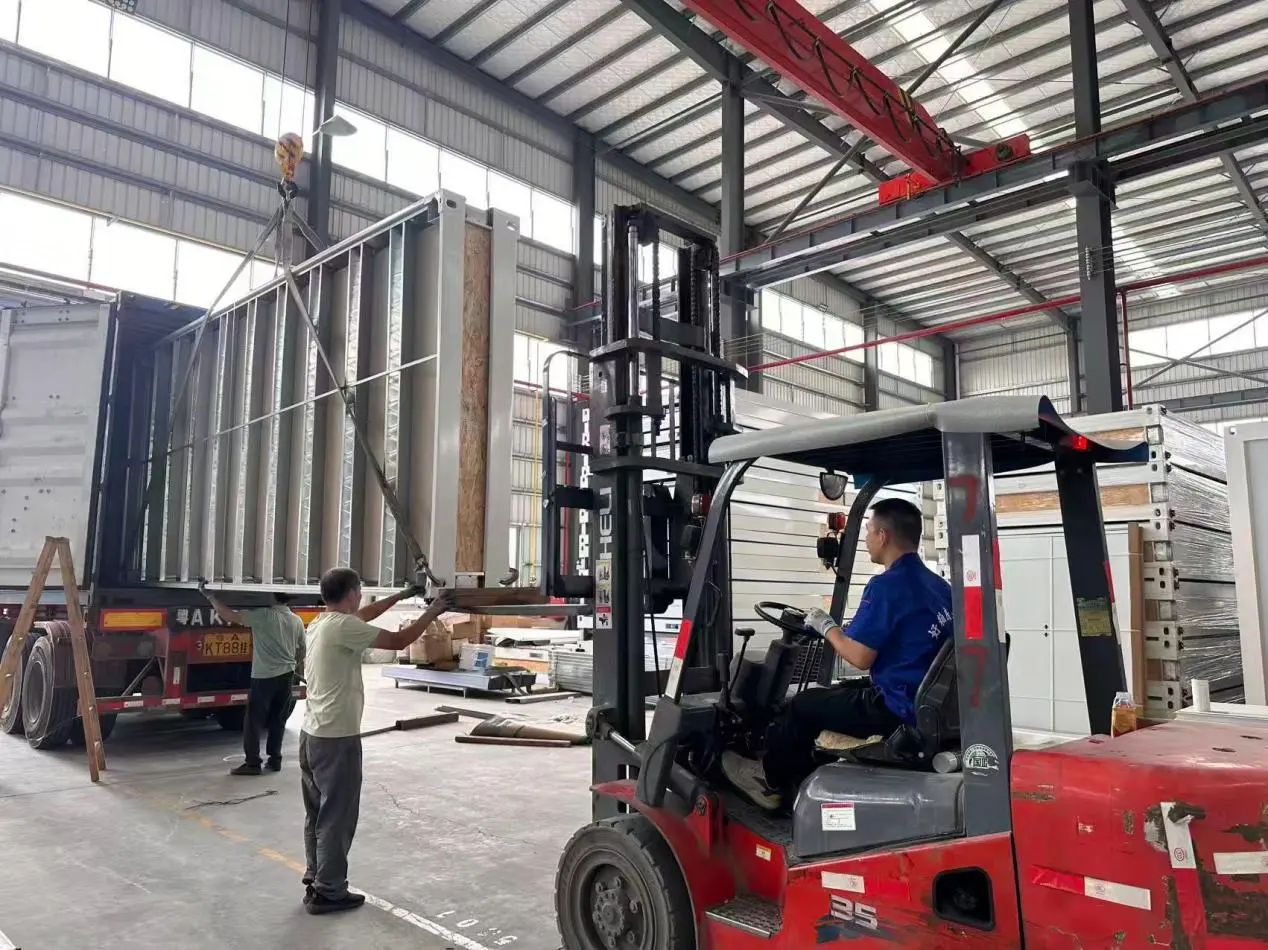
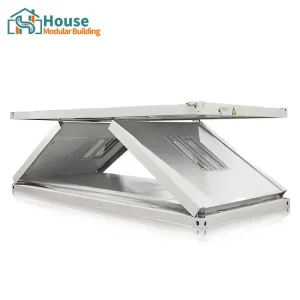
Our flatpack, collapsible, and expandable container configurations are specifically designed to pack efficiently into standard 40ft High Cube (HQ) shipping containers, reducing inland and sea transport costs per square meter.
One of the primary friction points in global modular procurement is conforming to local building codes, structural loads, and regional zoning certifications. House Modular Building actively addresses this by modifying core engineering parameters to align with international regulatory frameworks.
We work in tandem with local engineering consultants to tailor structural loads, seismic ratings, wind resistance values, and fire safety ratings. From the International Building Code (IBC) in North America to the Eurocodes in the EU, and the AS/NZS standards in Oceania, our engineers calculate the localized structural response models to guarantee compliance at the installation site.
Furthermore, our materials hold various international certifications, including CE, ISO9001, UL, and SGS, facilitating swift local customs clearance and final building occupancy approvals.
Our steel structures are engineered to withstand winds up to 120-150 km/h and resist seismic forces up to Zone 8. We utilize FEA (Finite Element Analysis) software to simulate local stress loads, ensuring structural stability over a 20+ year lifespan.
We adapt wall panels to target regional climate requirements. Insulation materials range from cost-effective EPS to flame-retardant Rockwool (for strict Class-A fire zones) and high-performance Polyurethane (PU) injection panels for sub-zero zones.
Mechanical, Electrical, and Plumbing (MEP) systems are integrated directly within the factory floor. Circuits, breaker boxes, and pipes are configured to local standards (UL for the USA, CE for Europe, and SAA/AS/NZS 3000 for Oceania).
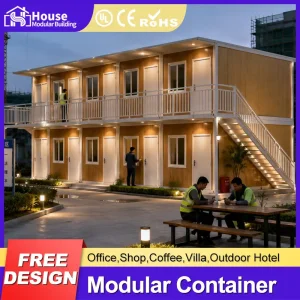
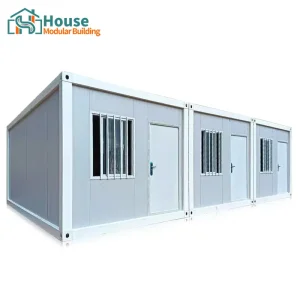
Custom manufactured container units are highly versatile structural elements. They serve as modern corporate workspaces, robust military and mining shelters, luxury commercial dining halls, and residential housing complexes.
Built for remote geological sites, our heavy-duty modular units serve as rugged worker camps, mess halls, and operations centers. These multi-unit structures withstand extreme temperature swings while offering comfortable interior living conditions.
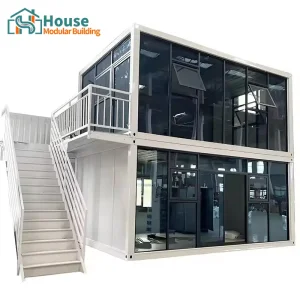
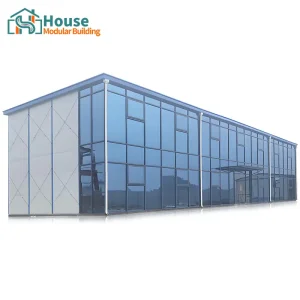
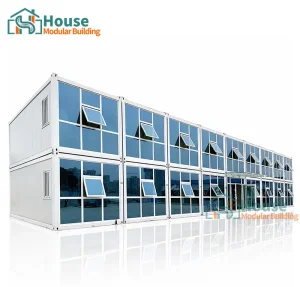
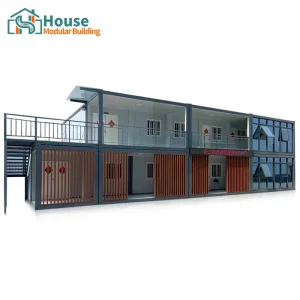
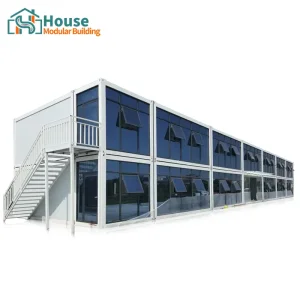
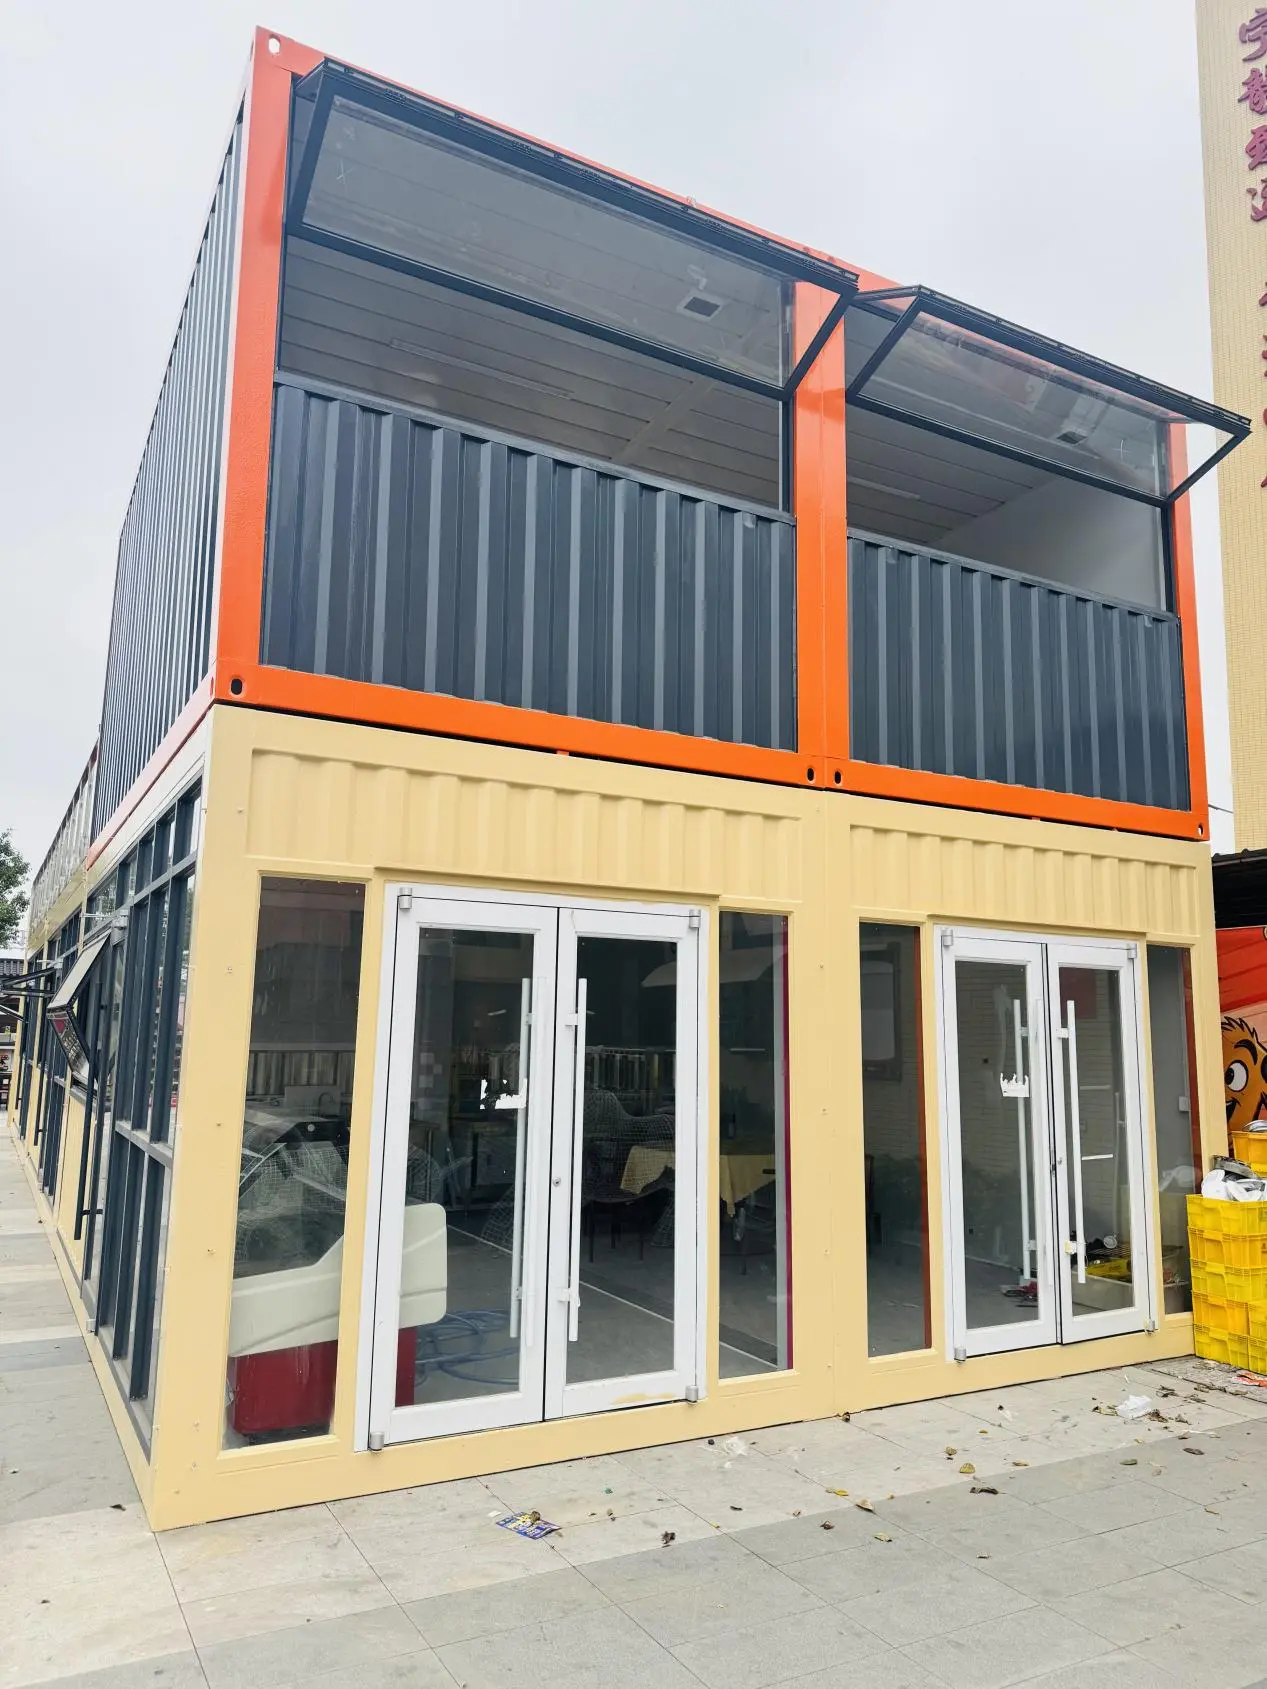
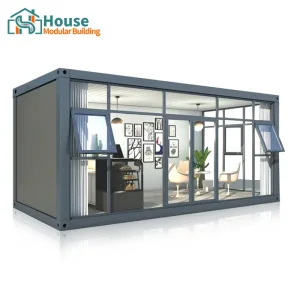
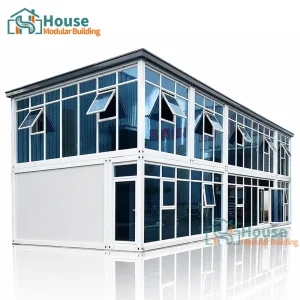
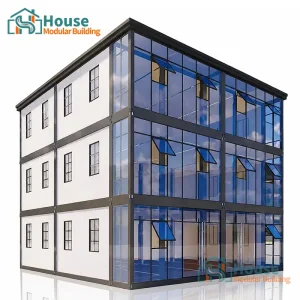
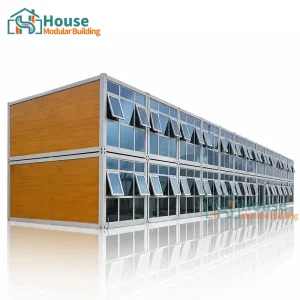
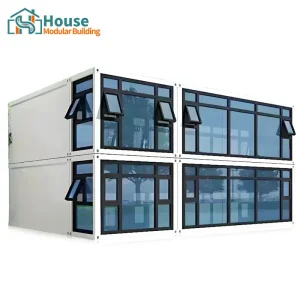
For corporate headquarters, real estate showrooms, and administration centers, we combine multi-story container structures with modern glass curtain walls. This architectural fusion creates open, well-lit spaces that can be deployed in a fraction of traditional construction timelines.
Pop-up cafes, convenience stores, and exhibition spaces leverage the inherent structural durability of modified shipping containers. These models are designed for fast mobilization, allowing commercial operators to open storefronts with minimal localized site work.
The global modular construction industry is experiencing rapid evolution driven by three primary challenges: labor shortages in traditional construction, strict carbon emission regulations, and the need for rapid deployment cycles.
Modern container modularity has evolved past simple emergency housing. Today, it represents a core pillar of eco-friendly green building practices. By manufacturing 90% of a building within a controlled factory environment, waste is reduced by up to 70% compared to traditional on-site construction.
Additionally, the adoption of circular economy principles ensures that steel modules can be disassembled, relocated, and repurposed at the end of their operational lifecycle. This makes manufactured container homes a preferred choice for companies aiming to meet ESG (Environmental, Social, and Governance) targets.
Our products are engineered to optimize international shipping container logistics. Modular units are shipped as flatpacks, collapsible packages (such as our Z-configuration collapsible container units), or pre-assembled structures. A standard 40ft High Cube (HQ) container can transport multiple flatpack modules, helping to minimize inland and sea freight expenses.
Yes. Our in-house engineering team works closely with global partners to adapt our structures to target local codes (such as IBC, IRC, Eurocodes, and AS/NZS). We adjust structural steel dimensions, load distribution calculations, electrical circuitry ratings, plumbing connections, and insulation ratings to match local regulatory frameworks.
We provide a variety of high-performance core insulation options, including Rockwool (highly favored for fire compliance and acoustic damping), expanded polystyrene (EPS), and polyurethane (PU) injection panels. We customize panel thickness to meet local thermal performance targets (R-values/U-factors).
Our heavy-duty hot-dip galvanized steel frames are treated to resist rust and corrosion. With proper foundation engineering and routine maintenance, our modular container homes and offices have an operational lifespan of 20 to 30 years.
Absolutely. As a production-focused factory enterprise, we provide white-label OEM and ODM manufacturing partnerships. We can custom-build to your local branding, interior design schemes, cladding requirements, and regional structural standards, offering a reliable supply chain to grow your regional brand.
 House Modular Building