The New Zealand construction sector is undergoing a massive structural shift. Driven by pressing housing shortages, surging material costs, and strict environmental directives, developers and commercial buyers are increasingly moving towards modular volumetric prefabrication. However, importing and deploying modular container houses in New Zealand is not a straightforward logistics exercise; it requires deep compliance with localized building standards, environmental considerations, and strict quality control pipelines.
From the seismic requirements under NZS 3604 to the rigorous thermal performance revisions in the NZBC Clause H1 Energy Efficiency framework, overseas manufacturers must possess highly specialized production capabilities. This guide presents an in-depth analytical breakdown of modular container factories serving New Zealand, details on global procurement, compliance roadmaps, and structural specifications engineered for local climates.
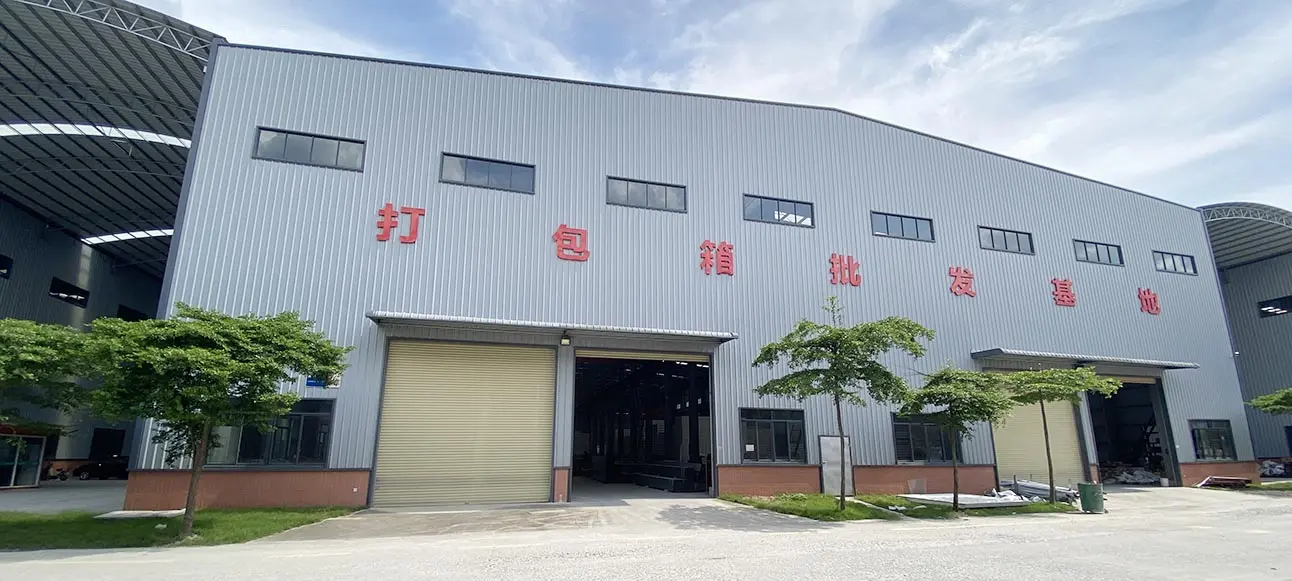
Engineered for compliance with local council regulations and optimized for rapid transport & deployment.
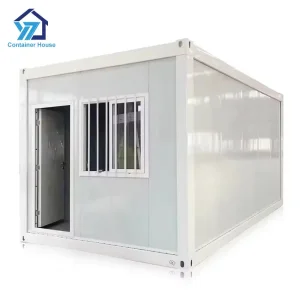
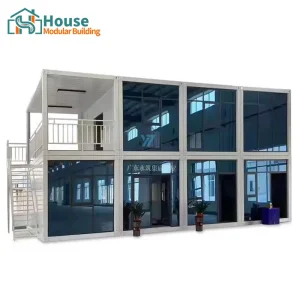
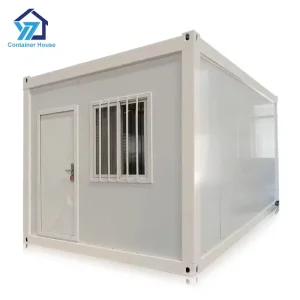
A comprehensive analysis of structural and thermal compliance indicators required under New Zealand building standards.
New Zealand is highly prone to seismic events. Standard containers must undergo structural reinforcements, integrating galvanized light-gauge steel frames (typically Q355B or G550 equivalent) welded to ISO corner castings. Wall studs, floor joists, and roof rafters are engineered to withstand dynamic loads in high-seismic zones like Wellington.
Recent changes to Clause H1 require significantly higher thermal performance (R-values) for building envelopes. In cold zones (e.g., Central Otago, Zone 6), roofs must reach R-6.6 and walls R-2.0 to R-3.2. To meet this, we use premium PIR (Polyisocyanurate) insulation sandwich panels combined with internal batts and thermal breaks to eliminate cold bridging.
Given New Zealand's long coastlines, marine atmospheric corrosion is highly aggressive (Category C4 or C5 under ISO 9223). We use hot-dip galvanized structural frames with a zinc coating thickness exceeding 275 g/m² (Z275) and finish with marine-grade protective coatings to prevent premature rust and degradation.
A detailed comparison outlining structural, time, and compliance features of different modular methods compared to conventional onsite framing.
| Feature | Traditional Timber Frame (NZS 3604) | Flat-Pack Container System | Fully Volumetric Steel Modular |
|---|---|---|---|
| Seismic Performance | Good (flexible but prone to deflection damage) | Excellent (independent rigid box frame) | Superior (welded structural steel chassis) |
| Onsite Construction Period | 6 - 12 Months | 2 - 5 Weeks | 1 - 2 Weeks |
| H1 Compliance Path | Onsite insulation installation (prone to gaps) | Factory-controlled PIR/Rockwool insulation | Integrated insulation with full thermal breaks |
| Corrosion Resistance | Subject to timber rot & moisture damage | Galvanized & coated (needs maintenance) | C4-M Marine-grade coating (long lifecycle) |
| Waste Reduction | High onsite construction waste (up to 30%) | Minimal (factory-cut material optimization) | Near zero (controlled industrial manufacturing) |
A leading factory-backed supplier delivering high-performance modular structures globally.
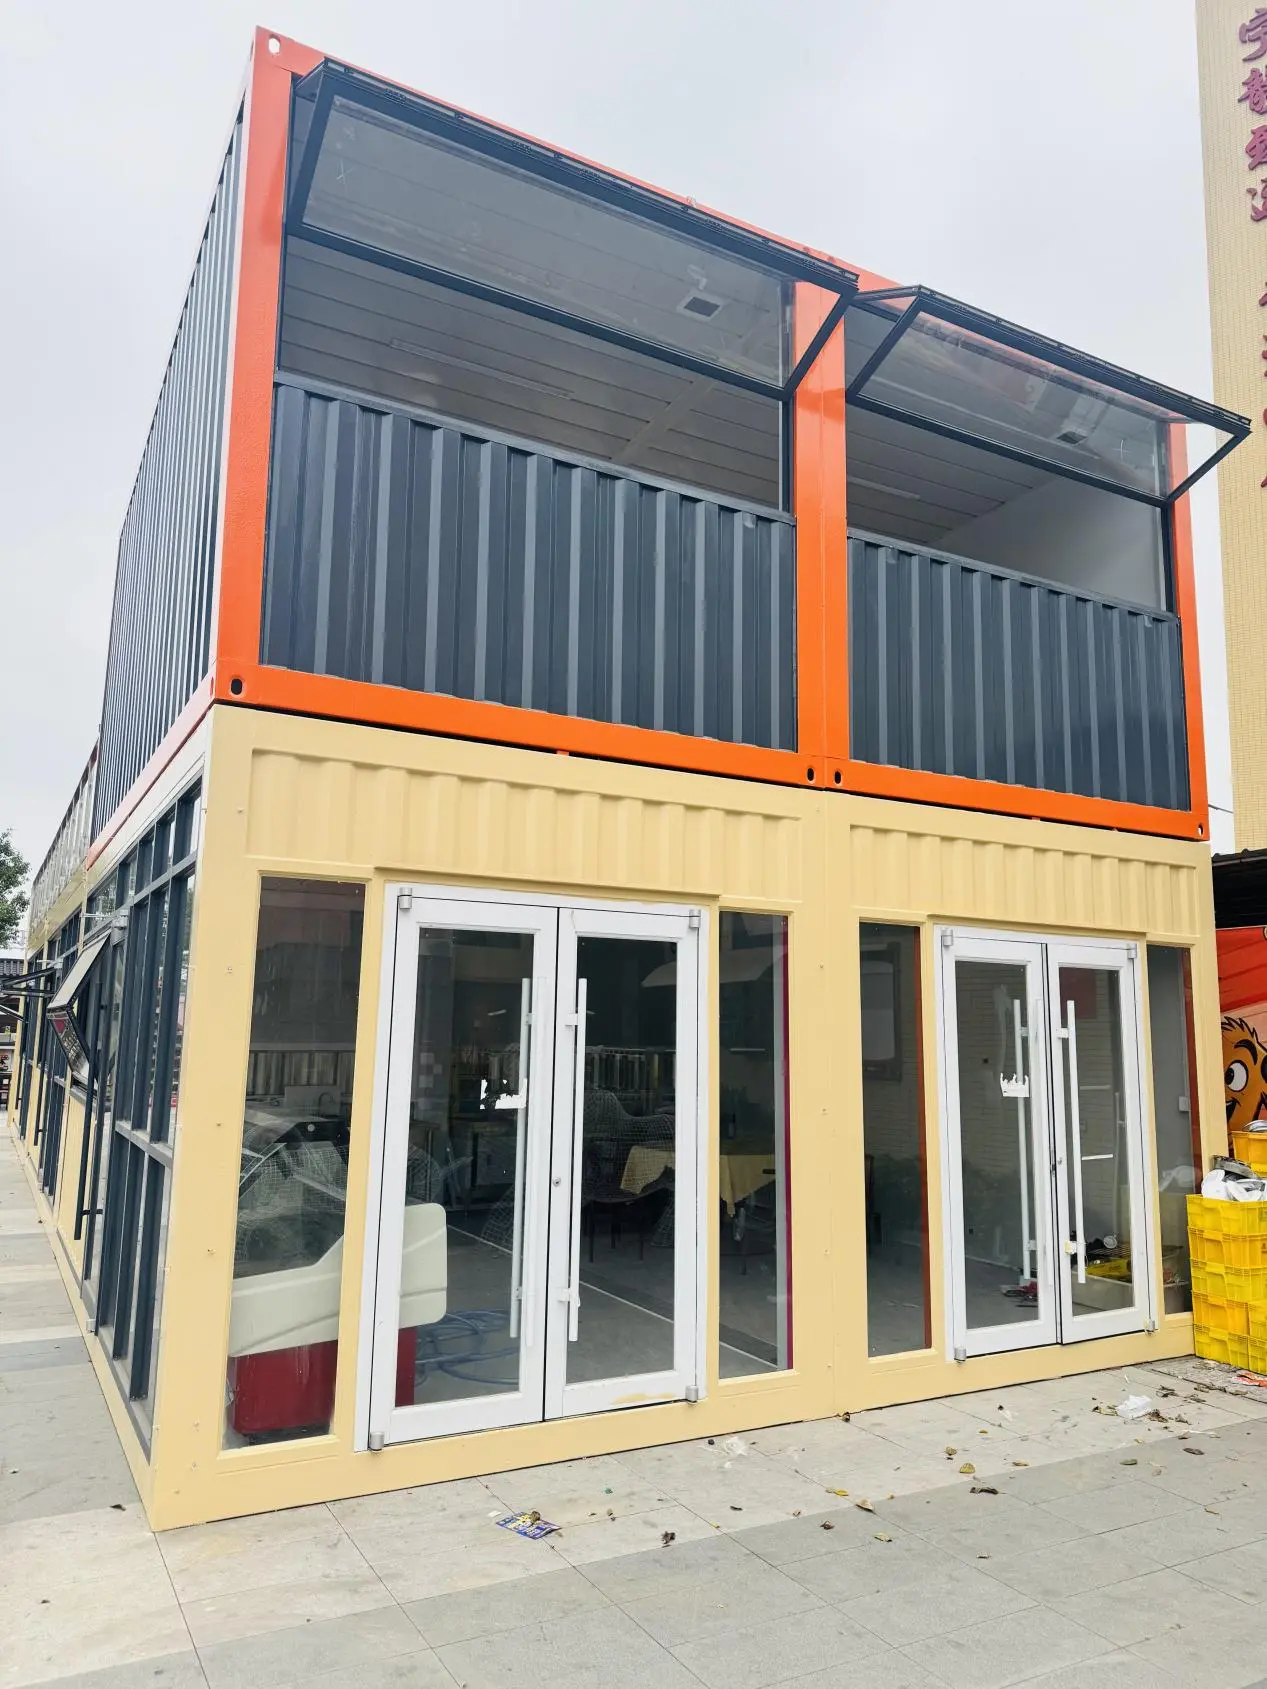
To better serve our international clients and demonstrate our production and delivery capabilities, House Modular Building has established production bases in both northern and southern China. This strategic layout provides efficient, cost-effective shipping lanes directly to major New Zealand ports, including Auckland, Tauranga, Wellington, and Lyttelton.
We support full OEM and ODM operations in our factories. For developers, construction firms, and distributors in Australia and New Zealand, we offer custom design consultation, compliance engineering, and localized support. Our dual-base model ensures that no matter where your project is situated, we can optimize shipping schedules and reduce container freight costs significantly.
Our company possesses comprehensive service capabilities spanning the entire product lifecycle—starting from raw material sourcing and structural testing to foundation drawings, delivery logistics, and assembly assistance. Our factory currently employs over 200 dedicated staff members, with our specialized research and development team accounting for more than 30% of our workforce.
Furthermore, over 60% of our production team members have more than 5 years of experience in the modular structures sector, and our core technical leads have operated in building materials service fields for over 10 years. This depth of expertise ensures every container leaves the line in accordance with exact customer specifications and relevant national standards.
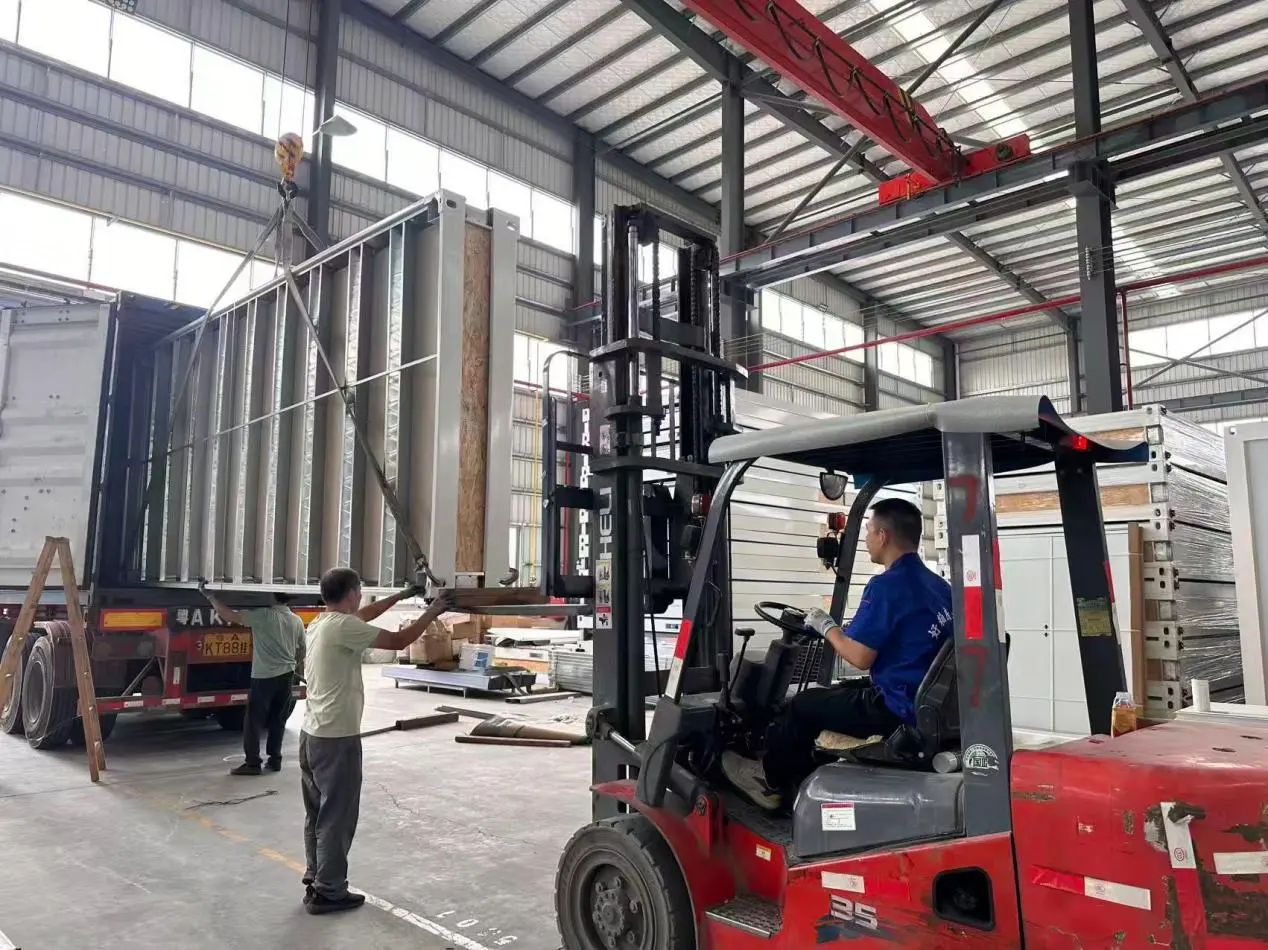
Minimizing lead times and mitigating import risks for commercial developers and distributors.
Our engineering team interfaces directly with your designers or LBP (Licensed Building Practitioner) in NZ to adapt plans for local consent. We specify local-equivalent structural members and confirm window/door apertures.
By standardizing high-stress connections, electrical wiring looms (complying with AS/NZS 3000), and sanitary plumbing configurations (complying with AS/NZS 3500), we guarantee quick installation times and passing marks on inspections.
Every modular unit undergoes a multi-point quality check including water tightness tests (simulating heavy rainfall), weld inspection, alignment testing, and electrical insulation tests before packaging and loading.
Premium architectural layouts, from glass curtain-wall offices to rustic eco-cabins.
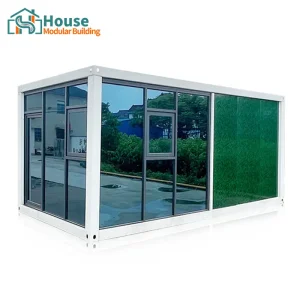
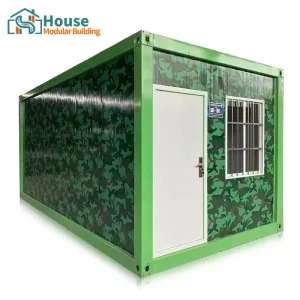
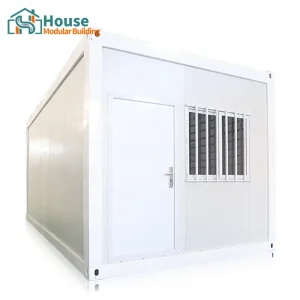
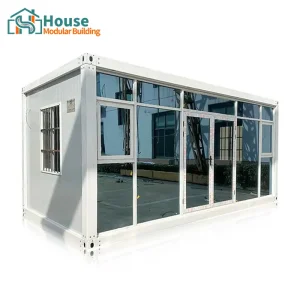
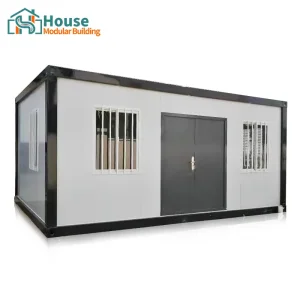
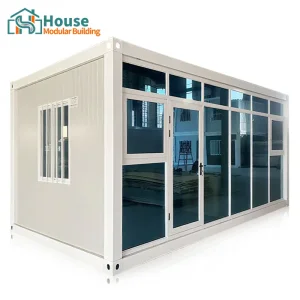
The next generation of prefabricated systems focusing on sustainability and carbon footprint reduction.
As the construction industry accounts for a substantial percentage of global carbon emissions, modular builders are integrating circular economy principles into their design processes. Using recycled steel structures and low-carbon insulation materials significantly lowers the embodied carbon footprint of each unit. Future iterations will focus heavily on life-cycle assessment (LCA) data to verify compliance with global ESG standards.
Additionally, we are exploring the standardization of off-grid solar kits, battery storage compartments, and greywater recycling loops directly built into the chassis. This makes the containers fully autonomous and highly attractive for remote settings, off-grid developments, and agricultural employee housing across rural areas of New Zealand.

Making sure that import processes go smoothly and meet all local certification frameworks.
We work alongside your local designer or consultant to prepare comprehensive manufacturer certificates, mill test certs, welding inspections, and thermal performance calculations. This ensures that the building consent application process with local district councils goes as smoothly as possible.
Imported structures must comply with AS/NZS 3000 (Electrical installations) and AS/NZS 3500 (Plumbing and drainage). We run specific cable paths and utilize certified materials, facilitating sign-offs by New Zealand-registered electricians and plumbers.
The Ministry for Primary Industries (MPI) in New Zealand has strict biosecurity standards regarding imported wood, packaging, and structural materials. We ensure all timber components (if utilized) are treated according to approved standards (e.g., H3.2/H5 treatment profiles) and accompanied by appropriate certificates to clear port checks.
Addressing the common regulatory, logistical, and design questions regarding modular houses in New Zealand.
 House Modular Building